

Expert MEP Products, always pushing boundaries
Advanced Detection & Automation Solutions
Designing and delivering reliable solutions for leak detection, environmental monitoring, smart automation, and infrastructure protection across commercial, industrial, and residential applications.
Our Product Portfolio
Liquid Leak Detection Sensors
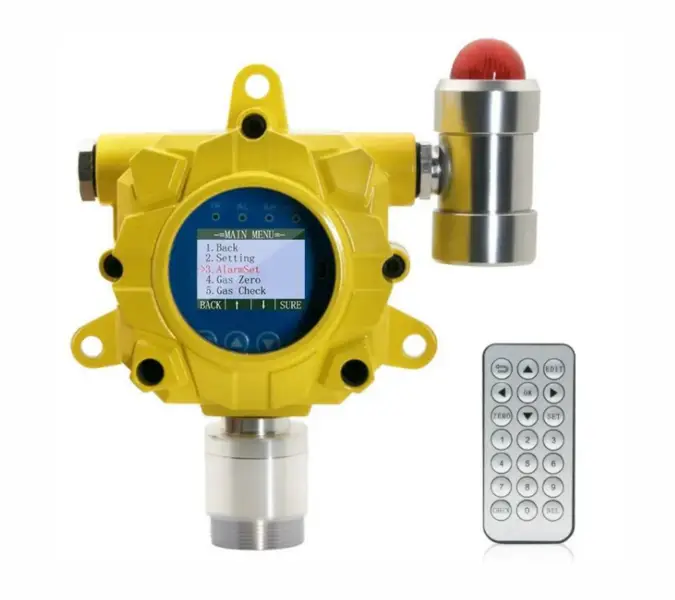
Gas Leak Detection Sensors
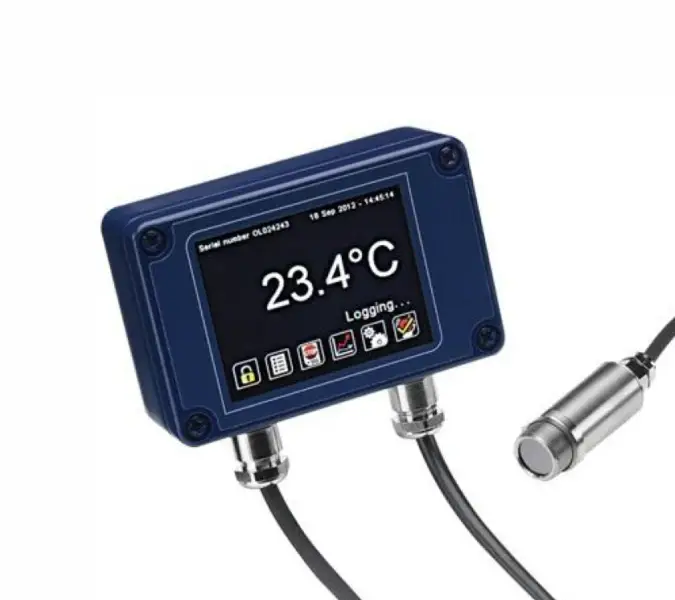
Temperature, Humidity & Moisture Control
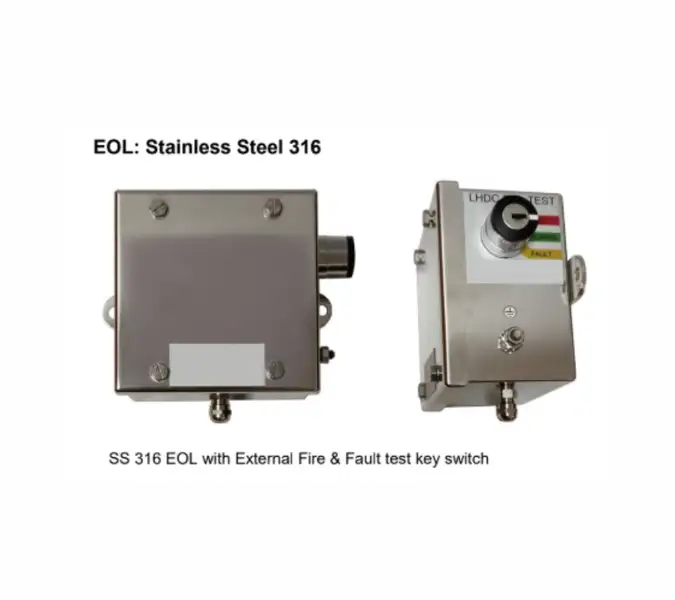
Linear Heat Detectors
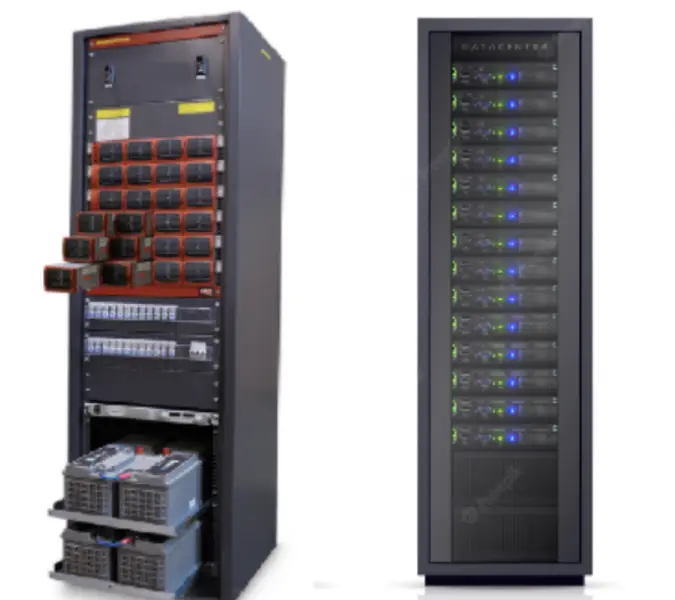
IT Hardware & Infrastructure
Smart Automation
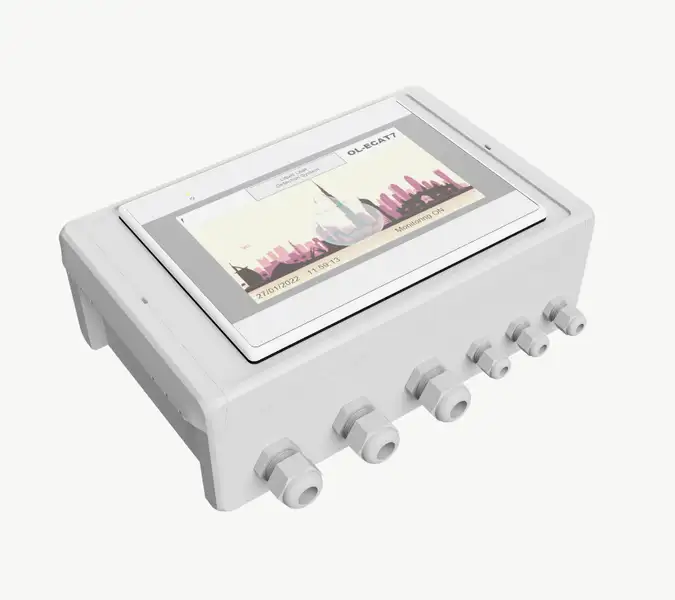
Liquid Leak Detection Sensors
Cutting-edge technology solutions engineered for reliability, precision, and seamless integration.
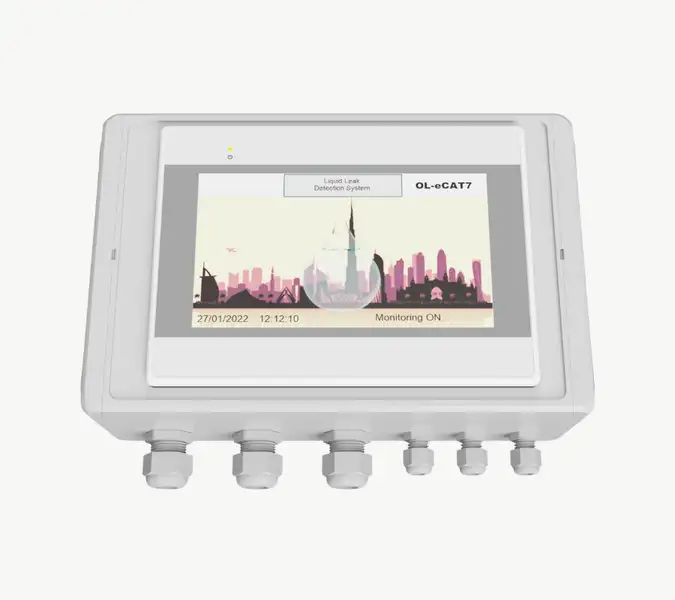
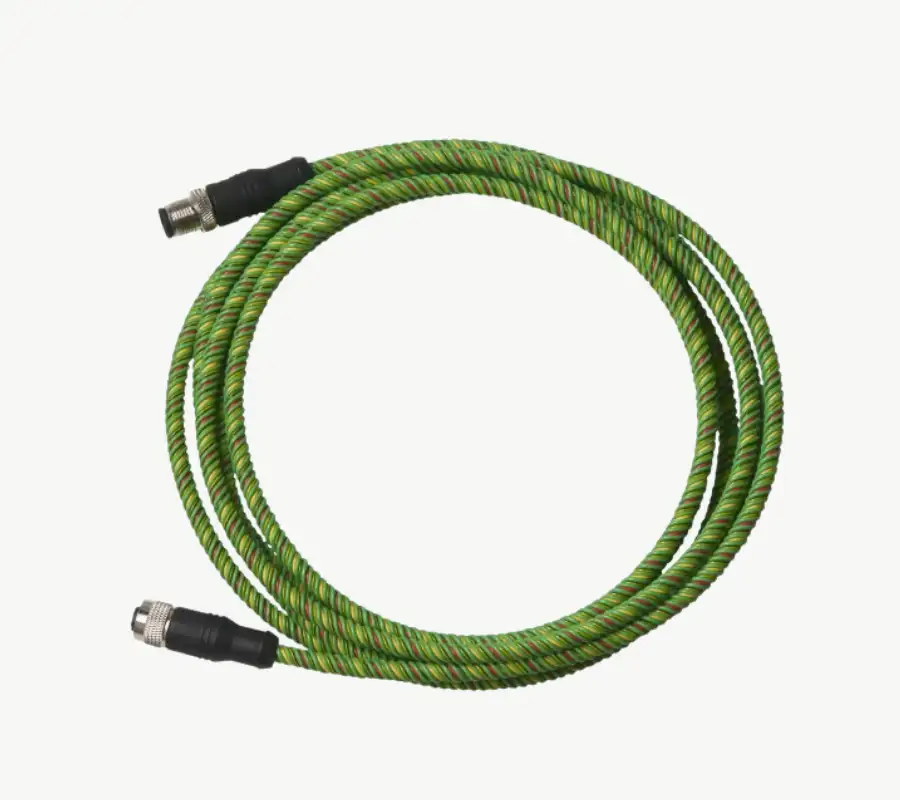
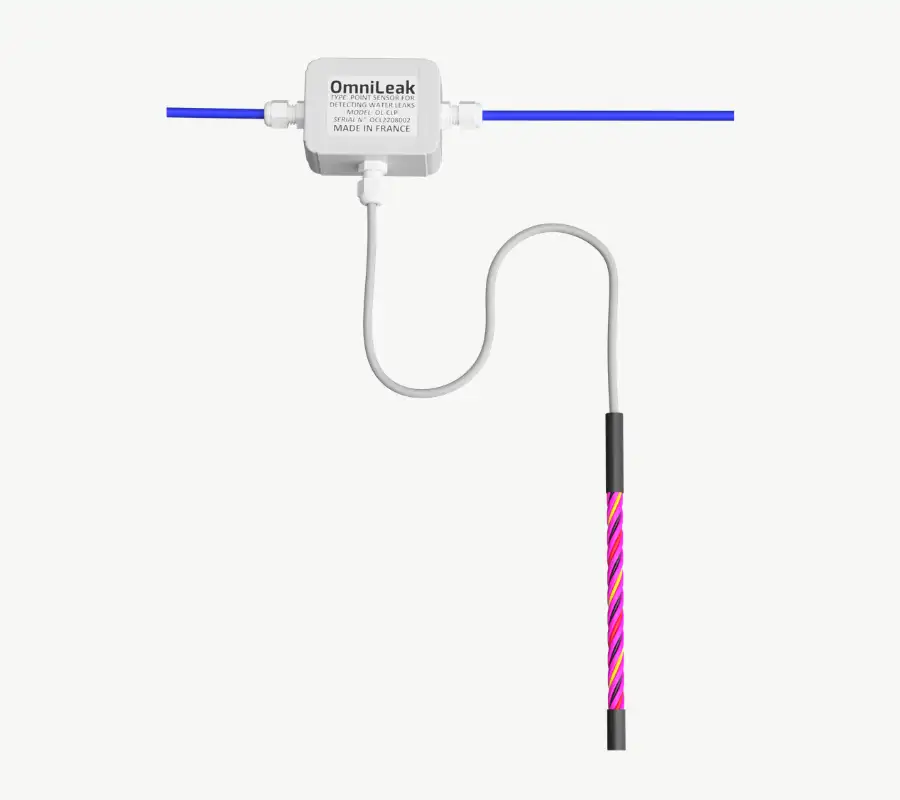
Advanced Leak Detection Technology
Monitors conductive and non-conductive liquids (water, acids, bases, naphtha, diesel, petrol, kerosene, fuels, hydrocarbons)
Redundancy loop-back monitoring even when cable is broken
Capable of monitoring deionized and NOVAC liquids
Touchscreen panel interface for easy operation
Certifications
ATEX, UL, ROHS, CE, IECEE, IECEx, NFPA, FCC
Hazardous Rating
Gas Leak Detection Sensors
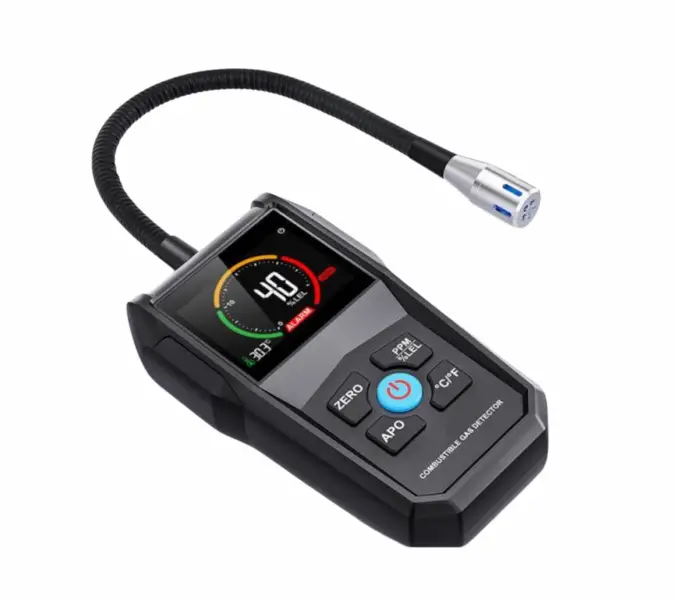
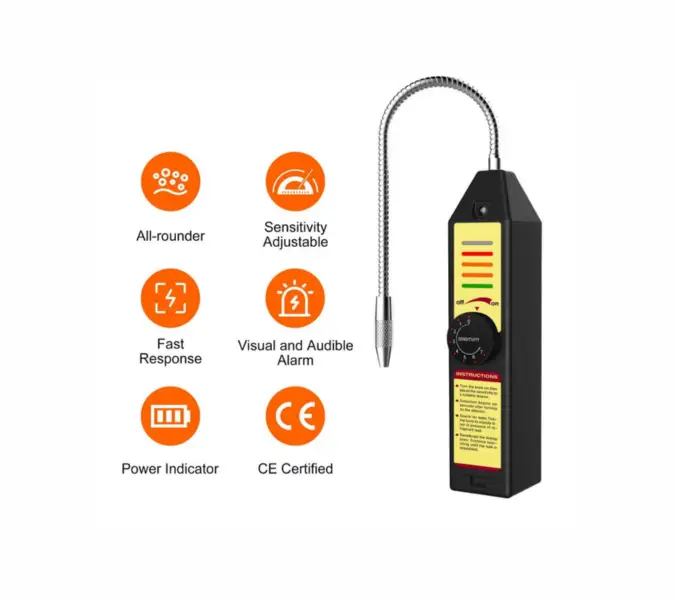
Multi-Gas Detection Capabilities
Refrigerant Sensors: Advanced detection for halogen, CHC, HFC (134a), CFC, and HCFC refrigerants
Combustible Gas Detection: Natural gas, methane, and propane monitoring
Toxic Gas Monitoring: Carbon monoxide, carbon dioxide, and smoke detection
Technology Types
Applications
Linear Heat Detectors
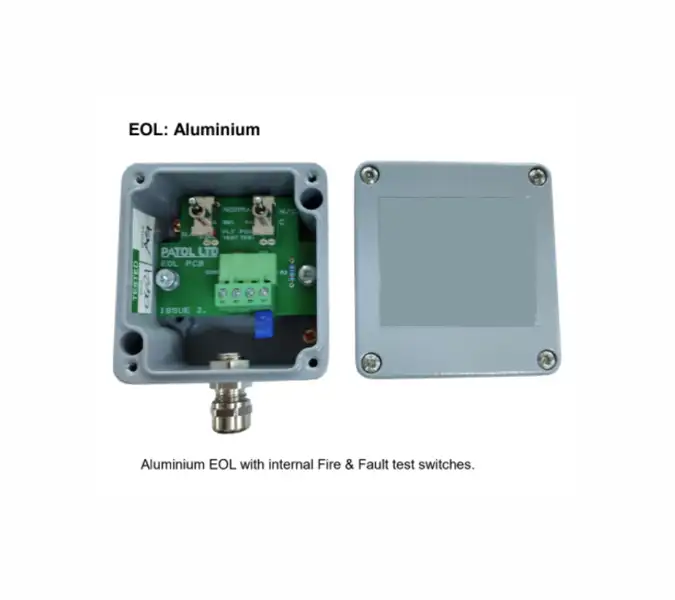
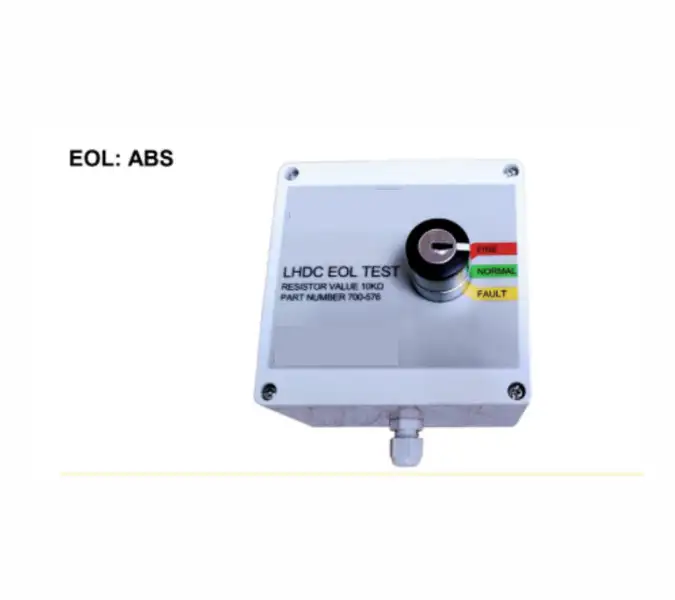
Advanced Fire Detection Technology
Linear heat detectors sense temperature increases along specific areas or pathways. They’re ideal for industrial and commercial settings where traditional point-type heat detectors don’t provide adequate coverage. Consisting of thermistors or thermocouples connected to monitoring systems, they detect heat generation typically from cable trays to enable quick action before fire occurs.
Continuous monitoring along entire cable length
Ideal for cable trays, conveyor belts, pipelines, and tunnels
Reliable and durable solutions for harsh environments
Early fire detection preventing catastrophic damage
Low maintenance with proven reliability
Sensor Type
Applications
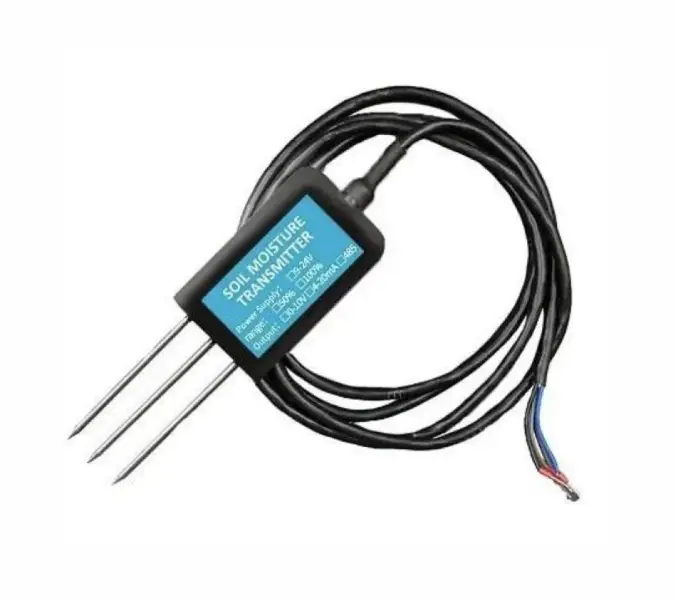
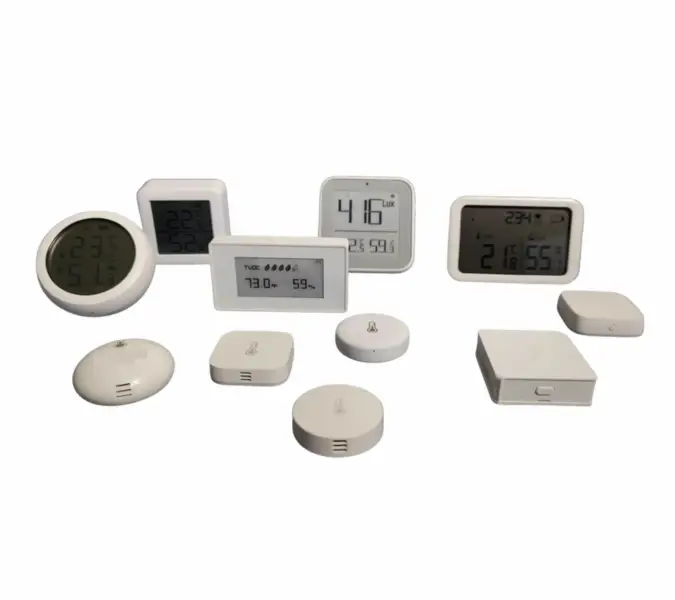
Temperature, Humidity & Moisture Control Sensors
Critical Environmental Monitoring
Real-time temperature and humidity monitoring for critical locations
Prevents equipment failure in data centers and manufacturing processes
Essential for incubators, respiratory equipment, sterilizers, and biological products
Optimizes HVAC systems and building comfort in smart buildings
Data logging and trending capabilities for analysis
Applications
Integration
Linear Heat Detectors
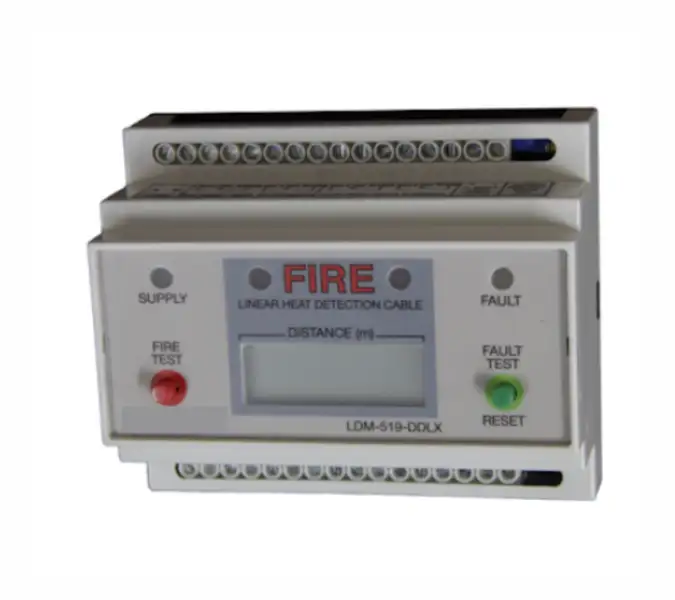
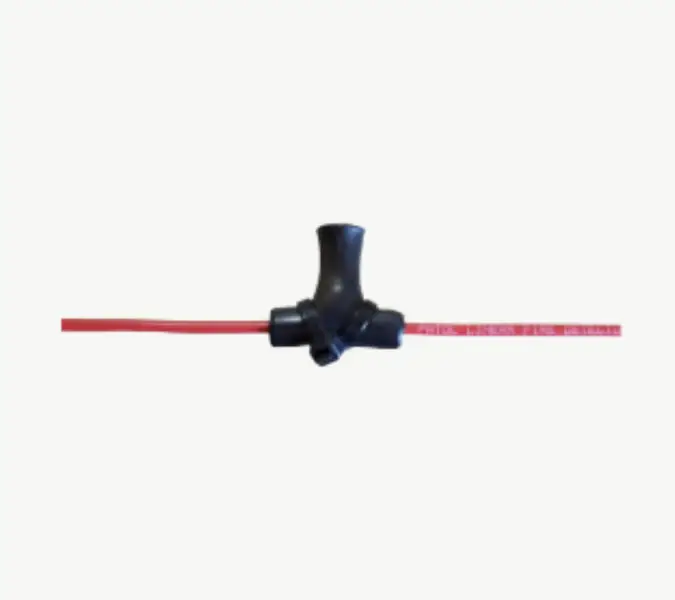
Advanced Fire Detection Technology
Continuous monitoring along entire cable length
Ideal for cable trays, conveyor belts, pipelines, and tunnels
Reliable and durable solutions for harsh environments
Early fire detection preventing catastrophic damage
Low maintenance with proven reliability
Sensor Type
Applications
IT Hardware & Infrastructure Solutions
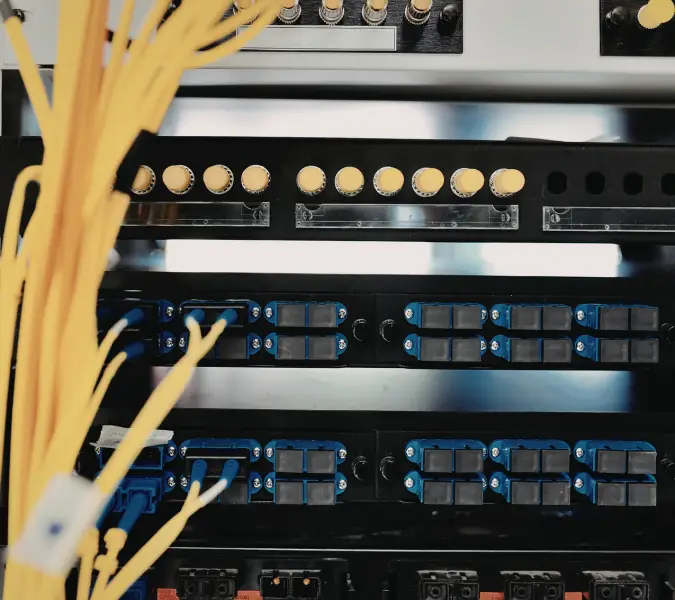
Complete IT Infrastructure
Data Center Infrastructure: Racks, cooling systems, and power distribution
Power Protection: UPS systems and backup batteries
Cloud Solutions: Hybrid and multi-cloud architecture
Networking: Switches, routers, and network security
Enterprise Servers & Storage: Scalable computing and data storage
Software Integration: Mobile applications and ERP systems
Complete Computer Supplies: Workstations, peripherals, accessories
Sensor Type
Applications
Smart Automation
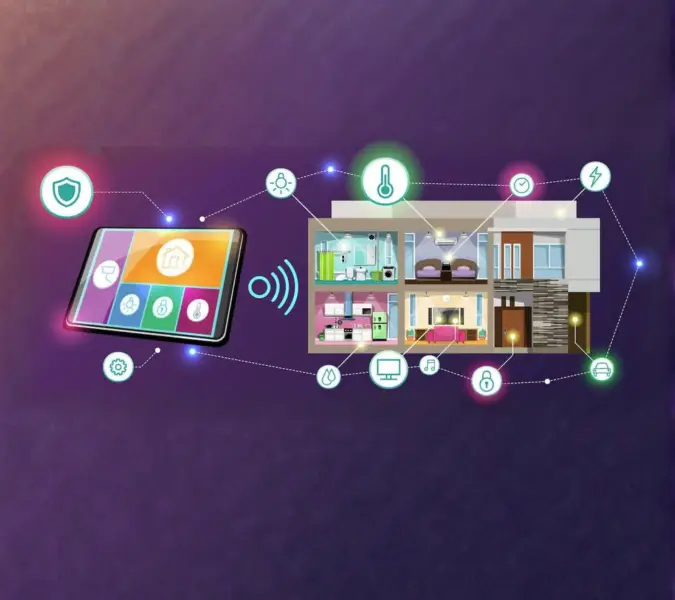
Intelligent Building Automation
IoT Solutions: Connected devices and sensors for comprehensive monitoring
AI Voice Control: Smart assistants for hands-free operation
Smart Devices: Intelligent thermostats, lighting, security systems
Energy Management: Automated optimization reducing consumption
Scene Control: Customizable automation scenarios
Applications
Also Suitable For
Perimeter Intrusion Detection
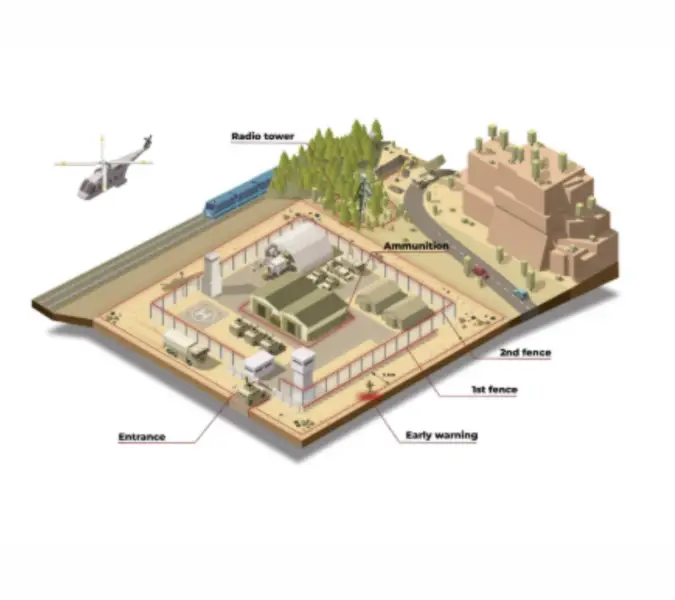
Military-Grade Security Systems
Suitable for harsh environments meeting military standards
Mobile deployment capability for field missions
Fully rodent-proof with highest mechanical performance
MIL standards compliant, NATO approved
End-to-end connectivity with field distribution units
EMC/EMP protected with lightning protection
Detects underground activities including tunneling
Invisible sensor with no EMC/EMI detection
Used by over 20 armed forces worldwide
Standards
Protection
Industry Applications
Healthcare
Data Centers
Manufacturing
Construction
Energy & Utilities
Education
Hospitality